Product Details
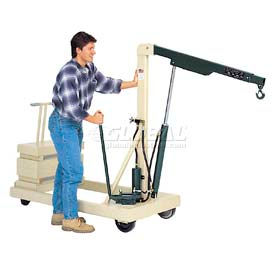
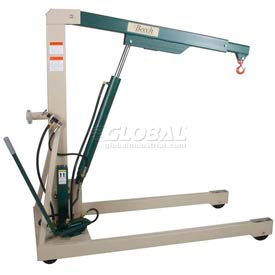
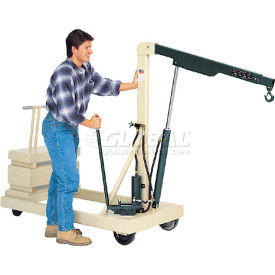
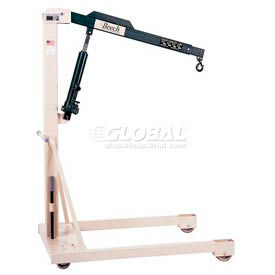
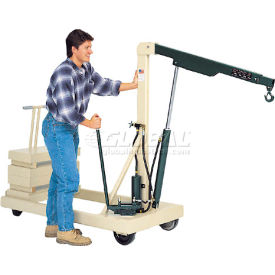
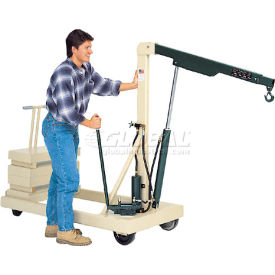
The reversed boom floor crane features a reversed boom design that eliminates front leg interference, allowing the crane to access, move under, and lift over obstacles in tight spaces. It provides safe and easy lifting in production areas and warehouses with a simple hand-operated hydraulic lift. The crane includes an integral overload relief valve and a needle valve that regulates lowering speed. Its alloy steel safety swivel hook and counterweight are included for secure handling. The unit is highly maneuverable with a rear-mounted tow handle and roller bearing phenolic wheels. It is factory tested to 150% of capacity and meets or exceeds ASME PALD-12 and ANSI Z-535 standards. The boom height range is reduced when the boom is retracted. The crane comes with a 2-year limited warranty.